2GR-FE Lower Manifold
Hux Racing "Over Port"
This page is to document 2GRFE lower intake manifold "over" porting process. We saw gains everywhere with significant improvement over 6500 RPM. In all our intake manifold tests we found that all the dyno charts had essentially the same results once you optimized runner length. This led me to believe the lower intake was the limit and that is how this test came about. 20whp at 7500 is a huge gain. This would look even better if this engine had the valve spring upgrade and could rev to 8500.

#4 intake test results

FMW V1 intake test results
Lets first get the lower intake porting naming system sorted.
1. Stock Lower = no rework done at all.
2. Ported Lower = removal of the injector bosses at bottom of intake. Removes restriction and increases CSA (cross sectional area} at manifold exit.
3. Fully Ported Lower=all listed above plus clean up of entire casting and slight enlargement of port. Port walls are very thin and you are limited in ability to enlarge the important areas.
4. Hux Racing Over Port=removal of injector boss , same as ported lower. No touching of port floor and minor side cleanup. Do not enlarge the entrance or exit of the port (other than injector boss). All 3 of the manifolds I modified had great port and manifold alignment as cast. The goal was straightening of the port roof to reduce the CSA change in the port and straighten the runner. I named this the "over" port due to the need to port beyond the thin casting walls.

Stock Lower Intake Injector Bosses

Ported Lower
Over Ported Lower pics and details below.
Watch these 2 videos first to understand what I did.


Completed Over Ported Lower Pics


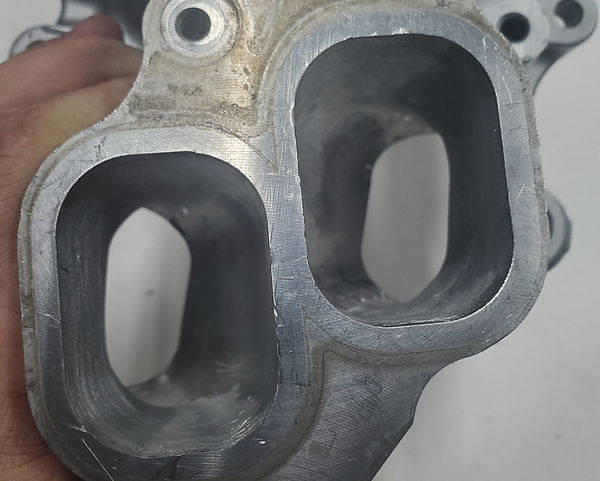
Showing how I picked where to pocket the port wall.

Slotting ports in a mill. You could do this with a drill and then use a grinder to connect the drilled holes.
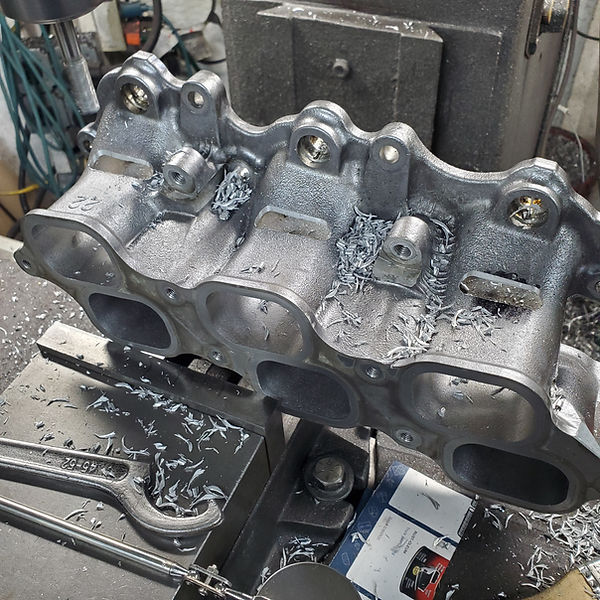
Ported wall down to sharp edge. I tapered from each end of the port.

Pic showing how thin areas where after grinding ports.

Aluminum piece I made to cover each port. I covered and bonded the entire side so that the thin wall could not break off and fall in.

I used JB weld to bond the covers down.

Finish port work after JB weld has cured.

You can see I did not touch the runner floor or completely finish the sides.


